Closing the Maintenance Execution Gap
Industrial companies have invested heavily in reliability engineering, preventive maintenance, condition monitoring and digitalisation. Yet many still struggle to realise the full value of those investments when they translate maintenance strategy into action on the machine.
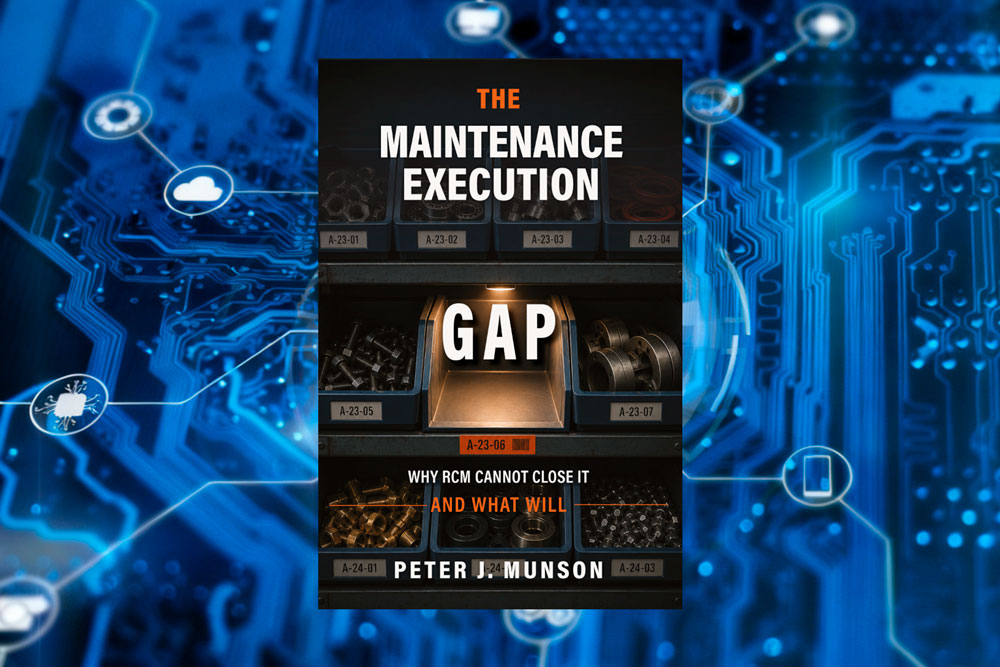
According to maintenance and reliability practitioner and author of The Maintenance Execution Gap: Why RCM Cannot Close It and What Will, Peter J. Munson, the problem is often not a lack of technology or analysis, but what happens when maintenance strategy is put into practice at the machine.
Munson calls this the maintenance execution gap: the distance between what a maintenance strategy intends to achieve and what reaches the equipment.
“The maintenance strategy of a company may be excellent,” Munson says. “However, what reaches the technician, the instruction, the tools, the right lubricant, access to the machine, and a way to report what was found, is usually a thin and degraded copy of it.”
The problem can emerge when reliability analysis is translated into work orders. A study may identify failure modes, maintenance tasks and intervals. Still, the resulting work instruction may contain little of the technical reasoning behind them – or the criteria for deciding whether equipment is operating as it should. Meanwhile, equipment changes while task lists remain untouched.
At one large plant Munson analysed, 91% of more than 19,000 equipment task lists were more than five years old, and none contained detailed instructions for carrying out the work.
One of Munson’s clearest examples of a vague maintenance instruction is: “PM pump. Check oil.”
It may satisfy a CMMS requirement, but what does it actually tell the technician? What constitutes acceptable oil condition? What temperature is normal? What should be measured? Which failure history matters? And what should the technician do if something is outside the expected range?
“An instruction like that gives the technician no acceptance criteria, no search sequence, no failure history for the machine and no rule for what to do when something looks wrong,” Munson says.
“So, he checks what his experience tells him to check, writes ‘Oil level OK, no issues,’ and closes the order.”
Without clear criteria and actions, the technician largely relies on personal experience.
Munson describes the result as a paradox: compliance can be 100%, while detection is zero. The CMMS records a completed preventive-maintenance task, but the inspection may have generated little or no useful information about the equipment’s condition.
A more effective instruction could specify an acceptance criterion and the required response – for example, a drive-end bearing temperature limit of 82°C, with notification and vibration analysis required if the limit is exceeded.
The difference is that technical knowledge has been translated into an actionable instruction rather than left buried in a report or dependent on someone’s memory and experience.
The challenge extends beyond maintenance instructions to the way maintenance performance is measured, Munson says. Completing a maintenance task does not necessarily mean it was effective.
Effectiveness requires additional evidence.
Traditional measures often focus on activity: Was preventive maintenance completed on time? Has the backlog decreased? Is the workforce being utilised?
Munson argues that the more important question is whether the work reduces risk, prevents degradation or restores performance.
“Good asset management requires system views and system outcomes,” he says. “Is our work effective in efficiently reducing risk and restoring performance to assets that naturally degrade?”
That is a key question when measuring maintenance performance.
One useful measure, he notes, is findings yield, the proportion of PM tasks that produce at least one actionable finding. Other measures include measurement completion – whether an inspection produces an actual measured value rather than simply “OK” – and detection rate, showing how many failures are identified before equipment loses its function. Munson notes that identifying a problem is only useful if you do something about it.
“A finding that sits in the backlog for six months is a finding the organisation has chosen to ignore,” Munson says.
Munson highlights that maintenance can also introduce failure mechanisms through incorrect installation, contamination, poor lubrication, inadequate tools, or uncontrolled fastening.
He points to examples such as improperly stored bearings, contaminated lubricants and components installed without appropriate torque or alignment controls.
These may not be individual technician failures but weaknesses in the maintenance system. If a defect appears shortly after a maintenance intervention, the organisation needs to recognise the connection. Otherwise, the resulting failure may be treated as another equipment problem.
“If the repair introduces the next defect, the plant has paid for faster diagnosis of a failure it is about to recreate,” Munson says.
Munson’s Maintenance Execution Framework looks at what must be in place for a maintenance strategy to work when it reaches the machine. The starting point is a practical question: when the technician arrives at the equipment, do they have the information, resources and conditions needed to do the job correctly? One part of the framework is what Munson calls an Execution Reference.
Rather than a generic instruction such as “PM pump. Check oil”, it should tell the technician what to look for, what constitutes an acceptable result and what to do if the result falls outside the expected range. Relevant failure history can also help the technician recognise recurring problems.
But good instructions are only one part of execution. The technician also needs the right tools, specified materials and lubricants, and equipment stored and prepared correctly. The machine must be safely accessible, isolated and permitted for work. If the job continues across shifts, relevant information and findings need to follow the work rather than being lost between handovers.
The framework also includes a feedback loop. Technicians should capture what they discover during maintenance and use it to improve future instructions, maintenance tasks, and decisions. In this way, field experience becomes part of the maintenance system rather than remaining with an individual technician.
The framework’s practical point is simple: a maintenance strategy is only as effective as the conditions that allow it to be executed correctly at the machine.
So how can companies close the maintenance execution gap? Munson recommends starting with the worst-performing assets rather than redesigning the entire maintenance system at once.
Take the last 20 completed PM tasks on a poor-performing asset. What was found? Did a finding generate a follow-up work order? Was it completed? Did the equipment perform better afterwards?
The investigation should also move beyond the CMMS and examine what happens at the machine. Are lubricants protected from contamination? Are the correct tools available? What happens when a technician reports a finding? At one plant Munson reviewed, nearly 70% of bad-actor locations had no PM at all.
He believes measurable progress can be made within six months by rebuilding Execution References for the top 10–20 bad actors and critical machines, adding findings yield and measurement completion to weekly maintenance discussions, improving lubrication practices and linking post-maintenance failures to the preceding job.
Munson says technicians should also receive feedback on what happened after they reported a finding. If a technician identifies a problem, they should know whether it was investigated, what action was taken and whether the action solved the problem. This closes the loop between inspection, maintenance and learning.
The maintenance industry has spent decades improving the analytical side of reliability. Munson argues that this knowledge creates value only when it reaches the machine in a form technicians can understand and act on, and when technicians’ field learning feeds back into the maintenance system.
Ultimately, reliability is not determined by the sophistication of an organisation’s analysis but by the quality of execution at the machine. The test is straightforward: does the maintenance system tell technicians what to do, give them what they need, and learn from what they find?
Four Ways to Close the Maintenance Execution Gap
• Focus first on your 10-20 worst-performing assets.
• Replace vague PM instructions with clear acceptance criteria and required actions.
• Measure findings yield and detection rate, not just PM completion.
• Link post-maintenance failures to the maintenance work that preceded them.
Peter J. Munson
Peter J. Munson is founder of SamOS Industrial Execution and has nearly 30 years of experience in maintenance, reliability and operations across industries including refining, chemicals, utilities and mining. A former U.S. Marine Corps maintenance officer and pilot, he holds CRE, CMRP and CRL credentials and is the author of The Maintenance Execution Gap: Why RCM Cannot Close It and What Will.
Text: Nina Garlo-Melkas Photos: Peter J. Munson
Subscribe to the free Maintworld newsletter here!